← Back to All Blogs
Inventory Management · 6 min read · Updated Aug 26, 2026
Material Handling Equipment Explained

TL;DR: Material handling equipment, forklifts, conveyors, pallet trucks, cranes, is what physically moves material around a factory. Choosing and using the wrong equipment for the actual volume and layout usually shows up as bottlenecks and damage, not as an obvious equipment problem.
This guide covers the main categories of material handling equipment used in manufacturing, how to match equipment to actual material flow, and where poor equipment choices quietly cost the most.
What Is Material Handling Equipment?
Material handling equipment covers the machines and tools used to move, store and control material as it moves through a factory, from receiving through production to dispatch.
The right equipment depends on what is being moved, how far, how often, and in what quantity, not a one-size-fits-all default.
Getting equipment choice wrong shows up as bottlenecks, damaged material, or wasted labor moving things by hand that should be mechanized, not as an obvious equipment failure.
Types of Material Handling Equipment
The Main Categories of Material Handling Equipment
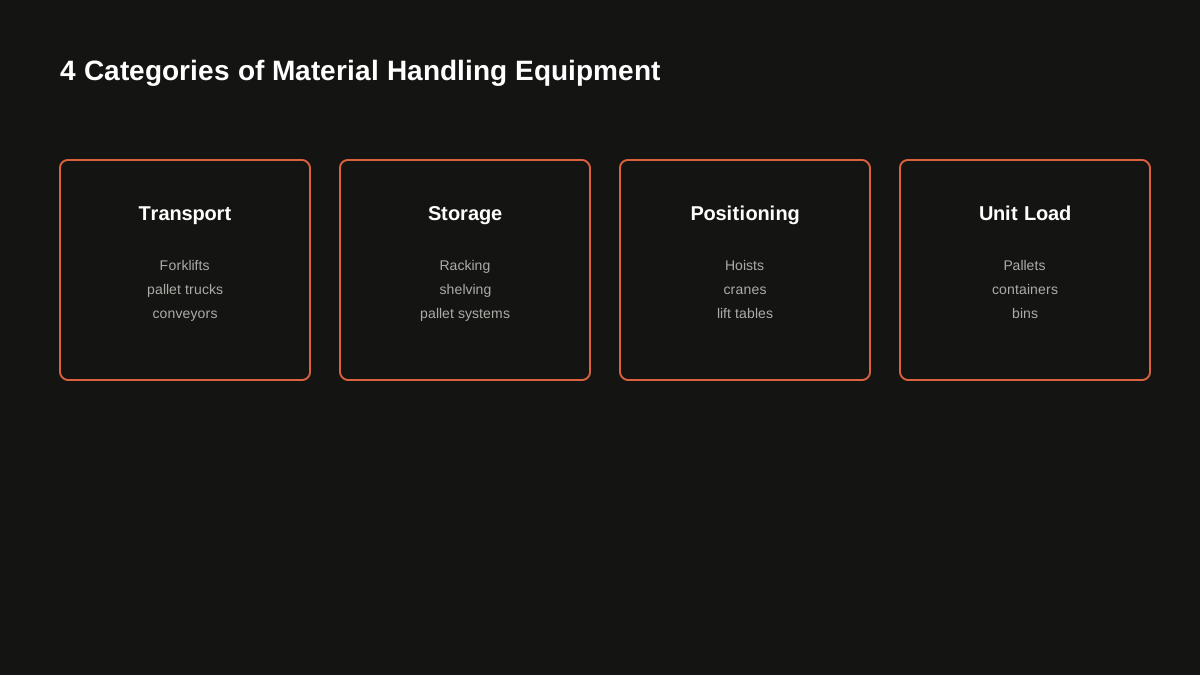
Almost every piece of material handling equipment in a factory falls into one of these:
Transport equipment. Forklifts, pallet trucks and conveyors that move material horizontally between stages or storage locations.
Storage equipment. Racking, shelving and pallet systems that hold material when it is not actively moving.
Positioning equipment. Hoists, cranes and lift tables that position heavy or awkward material for a specific process step.
Unit load equipment. Pallets, containers and bins that group material into a standard, movable unit instead of loose pieces.
Manual Handling vs Mechanized Handling
Speed: manual handling moves material at the pace of available labor; mechanized handling moves at the pace of the equipment, usually faster and more consistent.
Cost: manual handling has low upfront cost but ongoing labor cost and injury risk; mechanized handling has upfront equipment cost but lower per-move cost at volume.
Damage risk: manual handling risks drops and mishandling; mechanized handling, done correctly, moves material more consistently.
Scalability: manual handling does not scale past a certain volume without adding headcount; mechanized handling scales with equipment capacity.
Manufacturer relevance: the crossover point depends on volume, most SMEs run a mix, mechanizing high-frequency moves and keeping manual handling for low-volume, irregular ones.
Where Material Handling Equipment Choices Go Wrong
The same mistakes show up across manufacturing SMEs:
Undersized equipment for actual volume. A pallet truck rated for occasional use gets run at conveyor-belt frequency, breaking down faster than expected.
Manual handling where mechanization would pay off. Workers moving material by hand because the right equipment was never budgeted, at a real labor and injury-risk cost.
Equipment chosen without a real layout study. Buying a forklift that cannot maneuver the actual aisle widths in the warehouse.
No maintenance schedule. Equipment breakdowns stall material flow at the worst possible moment, mid-shift, with no backup.
Equipment mismatched to material characteristics. Using standard racking for material that needs cold storage or hazardous handling creates a compliance risk, not just an inefficiency.
Do you know which stage of your material flow is actually the bottleneck, or just which equipment looks the busiest?
TranZact doesn’t manage or track physical equipment, but warehouse-wise real-time stock tracking shows exactly where material needs to move next, the input equipment decisions should actually be based on.
See Real-Time Material Flow →
How TranZact Supports Material Flow Decisions
TranZact’s warehouse-wise real-time stock tracking shows which locations and materials actually see the most movement, the real data equipment and layout decisions should be based on.
It does not select, purchase or maintain material handling equipment for you. What it fixes is making sure that decision is based on real movement patterns, not a guess about which area looks busiest.
FAQs
What is material handling equipment?
Equipment used to move, store and control material as it moves through a factory, forklifts, conveyors, racking, hoists and unit-load containers like pallets and bins.
How do you choose the right material handling equipment?
Based on what is being moved, how far, how often, and in what quantity, matched against the actual warehouse layout, not a default equipment list.
What is the difference between manual and mechanized material handling?
Manual handling relies on labor to move material directly. Mechanized handling uses equipment like forklifts or conveyors, which usually costs more upfront but scales better at higher volume.
How often should material handling equipment be maintained?
On a scheduled basis matched to usage intensity, not just when something breaks, since an unplanned equipment failure mid-shift stalls material flow at the worst possible moment.
Does every factory need mechanized material handling equipment?
No. Low-volume or irregular moves are often cheaper to handle manually. Mechanization pays off once volume or frequency crosses a point where labor cost and speed limits start to bite.
Related Reading
Check out other blogs


Born in India. Building for the world.
Built by IIT & IIM founders
